Machine translation from Chinese. Check technical settings against the official parameter center.
¶ Product introduction
📖FusFun™ ABS-HF is a high-flow modified ABS filament supporting high-speed printing, with a maximum practical extrusion flow rate of up to 28mm³/s*. It releases less odor than ordinary ABS materials during printing, offers better anti-warping and crack-prevention capabilities, and exhibits excellent impact resistance.
*Test parameters: 12mm length copper heating block, BMG extruder, Phaetus hardened steel nozzle, nozzle size 0.4mm, layer height 0.2mm.
| Submission | Any tips, knowledge, experience, etc., that you find useful | Send to [email protected] |
| Correction | If you find any errors and omissions, the content is not limited to typos, descriptions, professional terms, solutions, etc. | Send to [email protected] |
| Copyright | Any copyright-related issues | Send to [email protected] |
¶ Product highlights & drawbacks
|
Application scenarios |
via ABS-HFOptimize flowability and reduce warping, making up for the printing difficulty of traditional ABS, making it suitable for a wider range of application scenarios. Compared to ordinary ABS, itSmoother printing, supports high-speed printing, more stable mechanical properties, especially suitable forLarge-size printing, automotive parts, electronic enclosures, industrial manufacturingand other fields. Although ABS-HF in Heat resistance, impact resistance, chemical resistance, and surface treatment capability Performs excellently in aspects, but still requiresHeated bed, enclosed printing environment, andNot resistant to long-term UV irradiation。 | |||
|
Highlights
|
High fluidity | High fluidity, supporting high-speed printing, smoother than traditional ABS printing, with a lower risk of nozzle clogging. | ||
| Low warping | ABS-HF has low insulation requirements and can maintain good adhesion to the build plate even when printed on an open-frame printer. | |||
|
Disadvantages |
Warping | Slight warping may still occur, it is recommended to use an enclosed printer and a heated bed. | ||
| Must be kept dry | Seal and use desiccant during storage to prevent degradation of printing quality. | |||
¶ 3D Printer hardware requirements & filament storage requirements
| Nozzle material requirements | Nozzles made of copper or higher-grade materials (diameter 0.2-1.0mm), supports hardened steel, stainless steel. |
| Recommended nozzle heating-zone length |
≥8mm The equipment printing temperature must be at least capable of reaching 250-280℃. |
| Sealing box | Recommended |
| Auxiliary chamber heating | Recommended |
| Heated bed heating |
Requires heated bed warming The heating temperature can reach 70-80℃ |
| Build plate material | PEI panel, glass, PC film or coating, PVP glue |
| Glue application instructions | For printing large models or models with small contact areas, it is recommended to apply PVP glue. |
| Filament Storage |
Direct external spool printing is not recommended (moisture absorption by moisture-proof filament causes stringing and print failure, resulting in poor print quality); it is recommended to use a bearing-equipped moisture-proof box for printing. If external printing is really necessary, please pay attention to whether some devices will interfere with the spool when mounted externally, causing extrusion obstruction and thus unsmooth filament feeding or jamming. |
| Auxiliary equipment (AMS/AMS2, Lite, etc.) | Supported. Regularly replace desiccants or check humidity levels to ensure proper moisture protection. |
| Moisture-proof |
*Immediately after first opening, place the filament in a moisture-proof box for use and keep the humidity below 15%. If it later absorbs moisture and print quality deteriorates, dry the filament according to the Wiki drying instructions. *Be sure to carefully read the drying precautions below before drying! Place in a 60-70℃ oven for drying for 4-6h! |
| Feed tube method (angle, bending, etc.) | Ensure smooth feeding |
¶ Printing setting parameters (recommended slicer software settings)
| Explanation of printing complexity | Relative difficulty is moderate; must keep dry; must ensure smooth feeding, Nozzles made of copper or higher-grade materials (diameter 0.2-1.0mm), supports hardened steel, stainless steel. |
| Nozzle temperature | 230-250℃ |
| Heated build plate temperature | 70-80 ℃ |
| Model cooling fan opening degree | 0 %-50 % |
| Retraction distance | 0.4-3 mm |
| Retraction speed | 30-60 mm/s |
| Recommended print speed | 30-200mm/s (In high-speed mode, the nozzle temperature can be set to 270℃) |
| Volumetric flow rate | 28mm³/s |
| Flow rate multiplier for testing | 0.95 (for testing purposes; in practice, it is recommended to select flow rate based on machine requirements through flow testing). It is recommended to disable the automatic flow calibration function. |
| Printing temperature for testing | 270 ℃ (for recommended printing temperature testing only) |
| K value | Bambu Lab devices default to 0.02. For other devices, refer to the manufacturer's recommended parameters. Please calibrate the values before changing them from the manufacturer's recommendations (if the deviation between the calibrated value and the manufacturer's recommendation is too large, consider recalibrating or contacting us for consultation). The K value affects print quality and success. |
¶ After printingAnnealing and resting requirements
| Annealing requirements | Meaningless |
| Resting requirements | None |
| Other | To better preserve filament that has not been used for a long time, please return it to the original aluminum foil packaging bag and add desiccant (such as silica gel packets or molecular sieves). Then, process by vacuum sealing and store in a cool place, avoiding direct sunlight, to ensure the filament remains in optimal condition. |
¶ Recommended support material
| Support material | FusFree™ S-Multi Quick-Remove Support |
¶ Download of print parameters (profiles)
Open the official print parameter center
The latest parameters and configuration files are maintained on the official website. Filter by material, slicer, printer model and nozzle size. Historical notes below are for reference; use the latest official configuration.
| Equipment Model | Nozzle diameter | Download address | File preparation slicing software | Update date |
| Bambu Lab X1C | 0.4mm | Open the official print parameter center | Bambulab Studio 1.9.7.52 | 20250102 |
¶ During printingStorage and filament moisture protectionRequirements
| How to position during printing |
The recommended placement scheme is shown in the figure below: 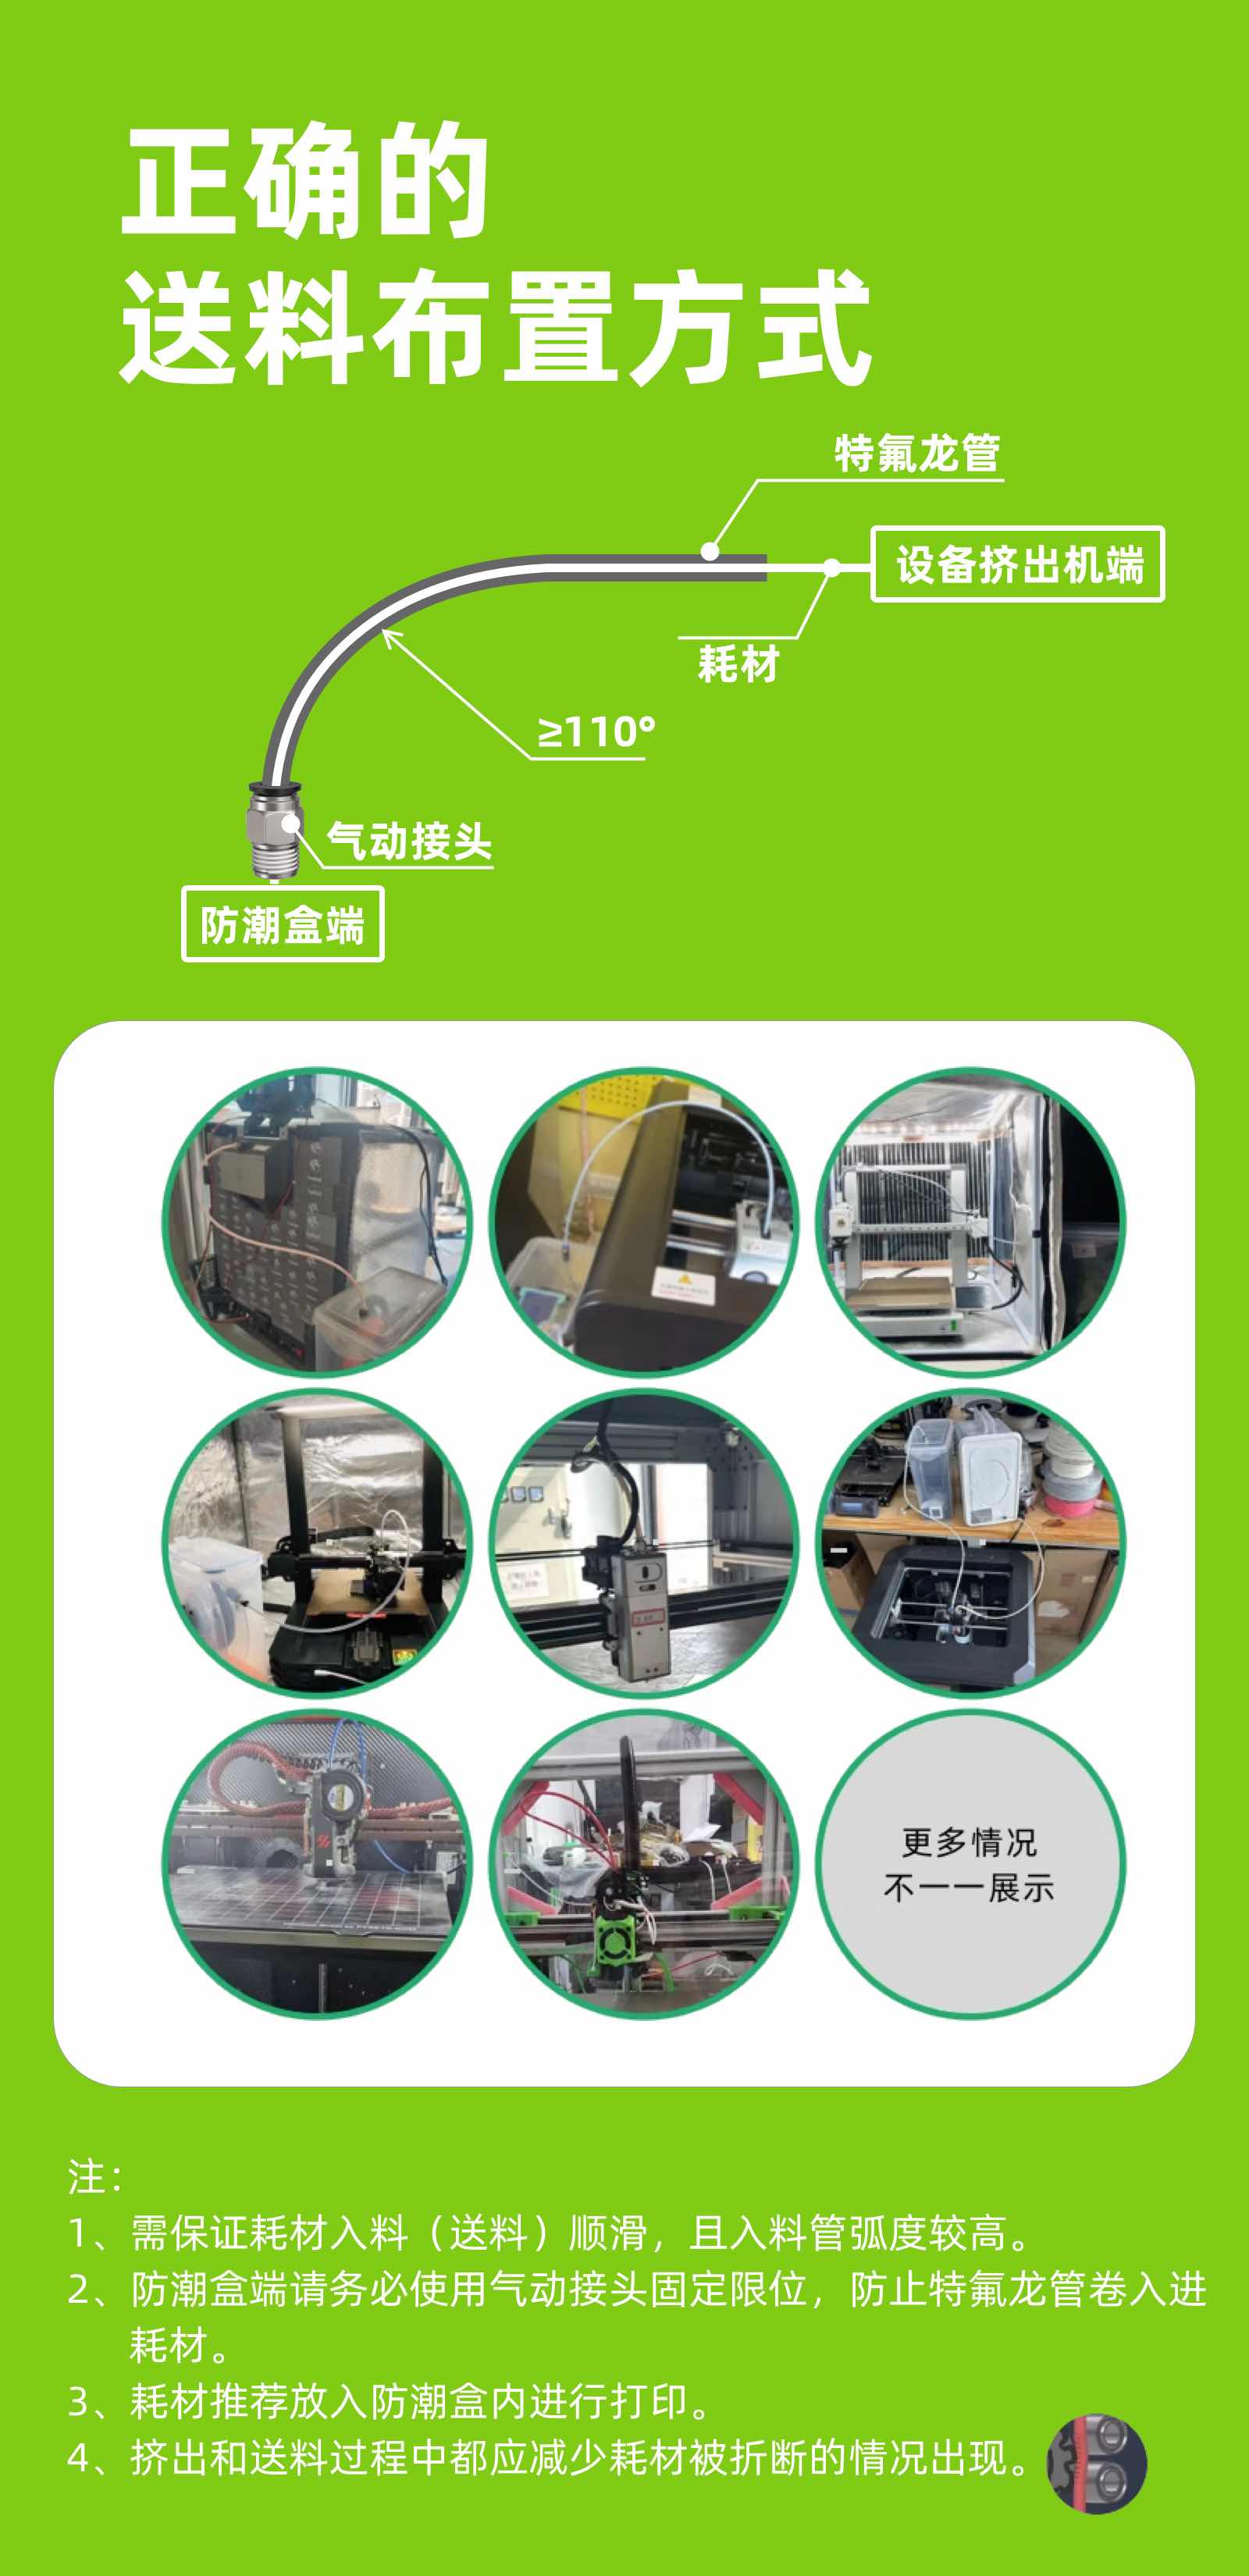 Use in conjunction with a moisture-proof box; ensure smooth feeding is guaranteed. It is recommended to use within a moisture-proof box equipped with bearings and feed the filament into the printer using a Teflon tube.
|
Direct external spool printing is not recommended (moisture absorption by moisture-proof filament causes stringing and print failure, resulting in poor print quality) If external printing is really necessary, please pay attention to whether some devices will interfere with the spool when mounted externally, causing extrusion obstruction and thus unsmooth filament feeding or jamming. (Solutions) 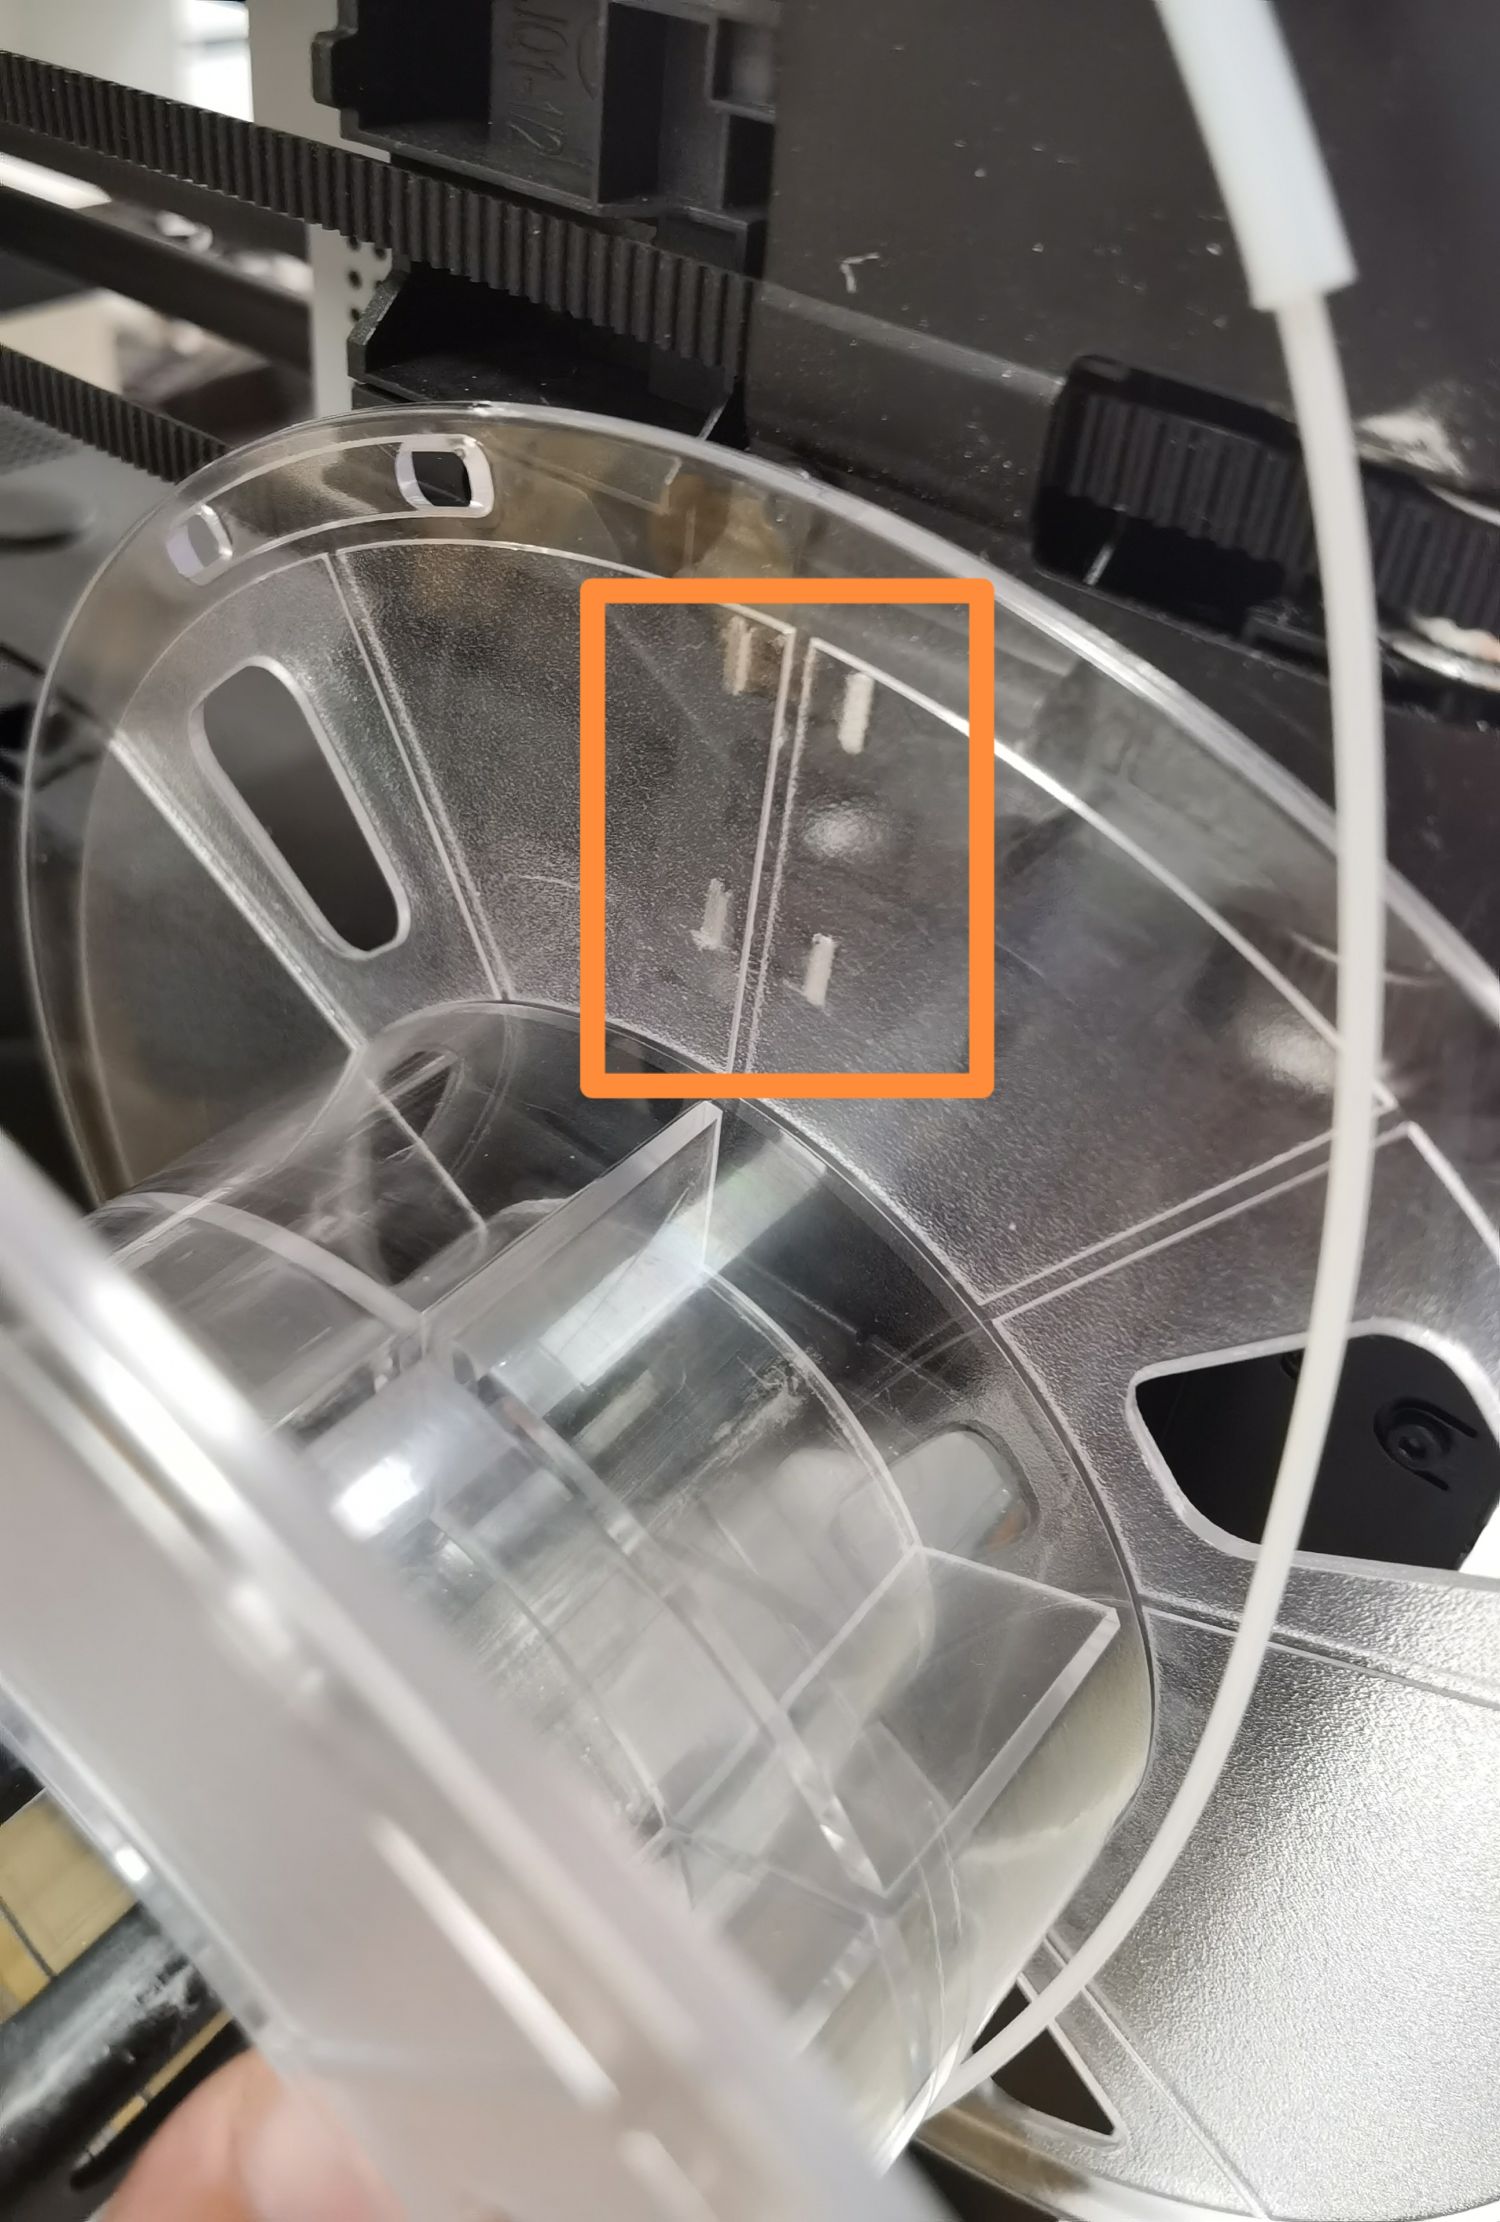
|
| Moisture-proof requirements |
1, replace desiccant in a timely manner to avoid situations where the filament acts as a desiccant, causing no change in the hygrometer reading. 2, ensure during printingMoisture-proof, place in a moisture-proof box, do not use commercially available heated moisture-proof boxes to heat while printing, which will accelerate material aging and may cause more severe filament moisture absorption due to inability to expel water vapor. 3 For printing with items placed in AMS/AMS2, pay attention to the humidity display status and replace desiccants promptly. 4 Dry the filament promptly if it has absorbed moisture. |
|
¶ Filament (moisture-proof) storage requirements
| when not used for a short time | 1, place in a sealed moisture-proof box or use simple vacuum sealing; avoid direct sunlight. | |
| Long-term non-use without moisture protection | 1, place the filament back into the original aluminum foil bag and remove the air from the bag (if possible, add a packet of dry desiccant inside). Then, place the bag inside a household vacuum-sealed storage bag and vacuum seal it. Store in a cool, dry place away from direct sunlight. | |
¶ Material properties table (physical, thermal, mechanical, impact properties)
| Physical properties | Test standard |
Typical numerical value |
|---|---|---|
|
Density |
ISO 1183 |
1.05 g/cm³ |
|
Melt flow index |
250°C, 2.16kg |
13 g/10min |
|
Thermodynamic properties |
Test standard |
Typical values for "Dry State" |
|
glass transition temperature |
ISO 11357 |
80 ℃ |
|
Heat deflection temperature |
ISO 75 Method A 1.80MPa |
65 ℃ |
|
ISO 75 Method B 0.45MPa |
72 ℃ |
|
|
The general heat deflection temperature is related to the environmental pressure or load on the material. Therefore, according to ASTM D648 or ISO 75-1, -2 standards, the material will be tested under 0.45MPa (simulating no pressure load) and 1.80MPa (simulating a certain pressure load). The heat deflection temperature of the material under two different pressures, in order to better describe the thermodynamic properties of the material. Generally, the heat deflection temperature obtained under 0.45MPa is higher than that obtained under 1.8MPa. |
||
|
Mechanical properties |
Test standard |
Typical values for "Dry State" |
|
Tensile fracture strength (X-Y) |
ISO 527 |
37.13±0.59 MPa |
|
Yield elongation (X-Y) |
2.32±0.07 % |
|
|
Young's modulus (X-Y) |
2115.10±24.02 MPa |
|
|
Tensile fracture strength (X-Y) |
30.29±2.28 MPa |
|
|
Elongation at break (X-Y) |
3.65±1.52 % |
|
|
Tensile fracture strength (Z) |
ISO 527 |
33.48±0.23 MPa |
|
Young's modulus (Z) |
2097.03±37.77 MPa |
|
|
Elongation at break (Z) |
4.07±0.57 % |
|
|
Flexural strength (X-Y) |
ISO 178 |
57.46±0.25 MPa |
|
Flexural modulus (X-Y) |
2117.02±32.46 MPa |
|
|
Impact performance |
Test standard |
Typical values for "Dry State" |
|
Notched impact strength (X-Y) |
ISO 179 |
23.16±2.32 KJ/㎡ |
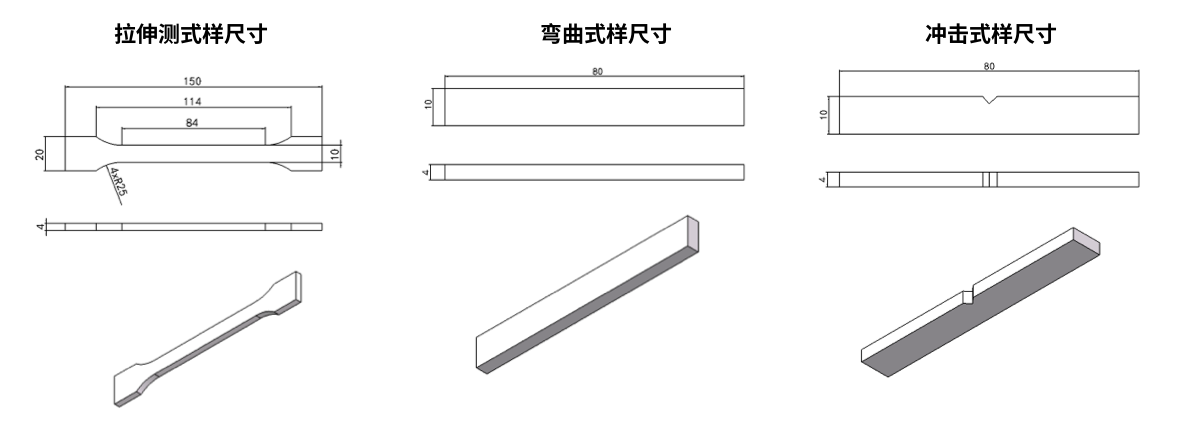
| Sample Printing Parameters: Nozzle size 0.4mm, nozzle temperature 250°C, build plate heating 80°C, print speed 50mm/s, infill rate 100%, infill angle ±45°. | ||
 |
||
*For crystalline materials, the Vicat softening temperature and melting point temperature are not significantly different, so relevant testing was not conducted.
Interpretation of Common Filament Performance Parameters
¶ Solutions and methods for handling moisture-absorbed filament
| Drying parameters |
PTC Small Drying Box: 60-70℃, Dry for 4-6 hours Small constant-temperature drum dryer: This filament reduces 20 degree to avoid deformation caused by uneven temperature distribution in small equipment (40-45℃, dry for 4 hours),If there is no improvement in printing effect after drying at this temperatureFirst perform a temperature test with an empty spool before increasing the drying temperature, to prevent deformation of the spool due to excessive or uneven temperatures. Large constant-temperature drum dryer: 60-70℃, dry for 4-6 hours PS: Why do different drying equipment have different drying temperatures: Click to view |
| Precautions⚠️ |
1, if unsure, first perform a temperature test using an empty spool to prevent deformation of the spool due to excessive or uneven temperatures during drying. 2, strictly follow the drying temperature and time recommended on the filament parameter introduction page. 3 Drum dryers are recommended (do not point directly at the air outlet! Otherwise, deformation will occur) 4 When drying the spool, avoid the air outlet. 5 It is not recommended to place the spool directly on a mesh (it is recommended to use a flat plate such as a metal plate). 6 Be careful of burns due to high temperature when removing filament. 7 Prevent fire and pay attention to equipment safety. 8 Note: When drying filament, printed parts, and annealing printed parts, it is recommended to use equipment with uniform temperature, such as a forced-air oven (Blast drying oven) (some manufacturers' substandard products cannot be used). Do not use microwaves or household ovens. Avoid significant stress or uneven heating (must stay away from the oven's heating zone) to prevent damage to filament, spools, or models due to local overload or overheating. 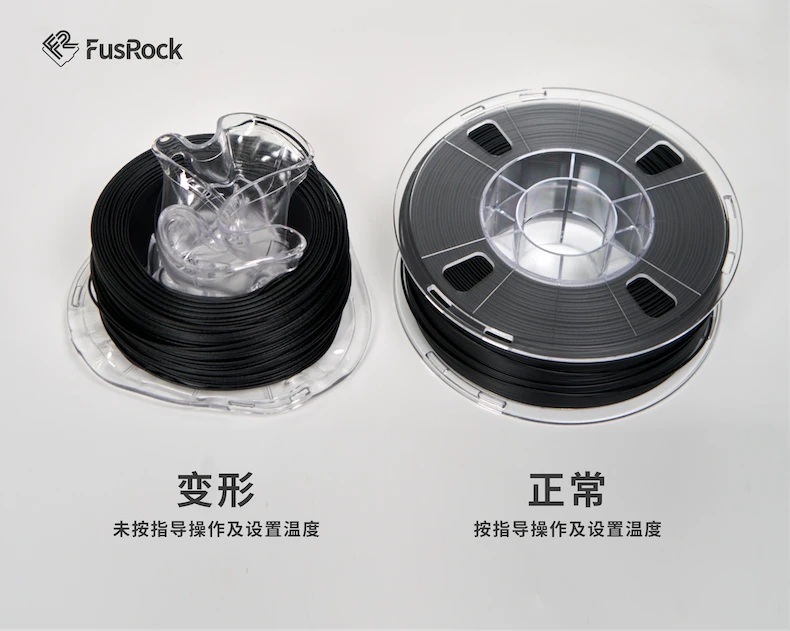 |
| Comparison of dried vs. moisture-absorbed states |
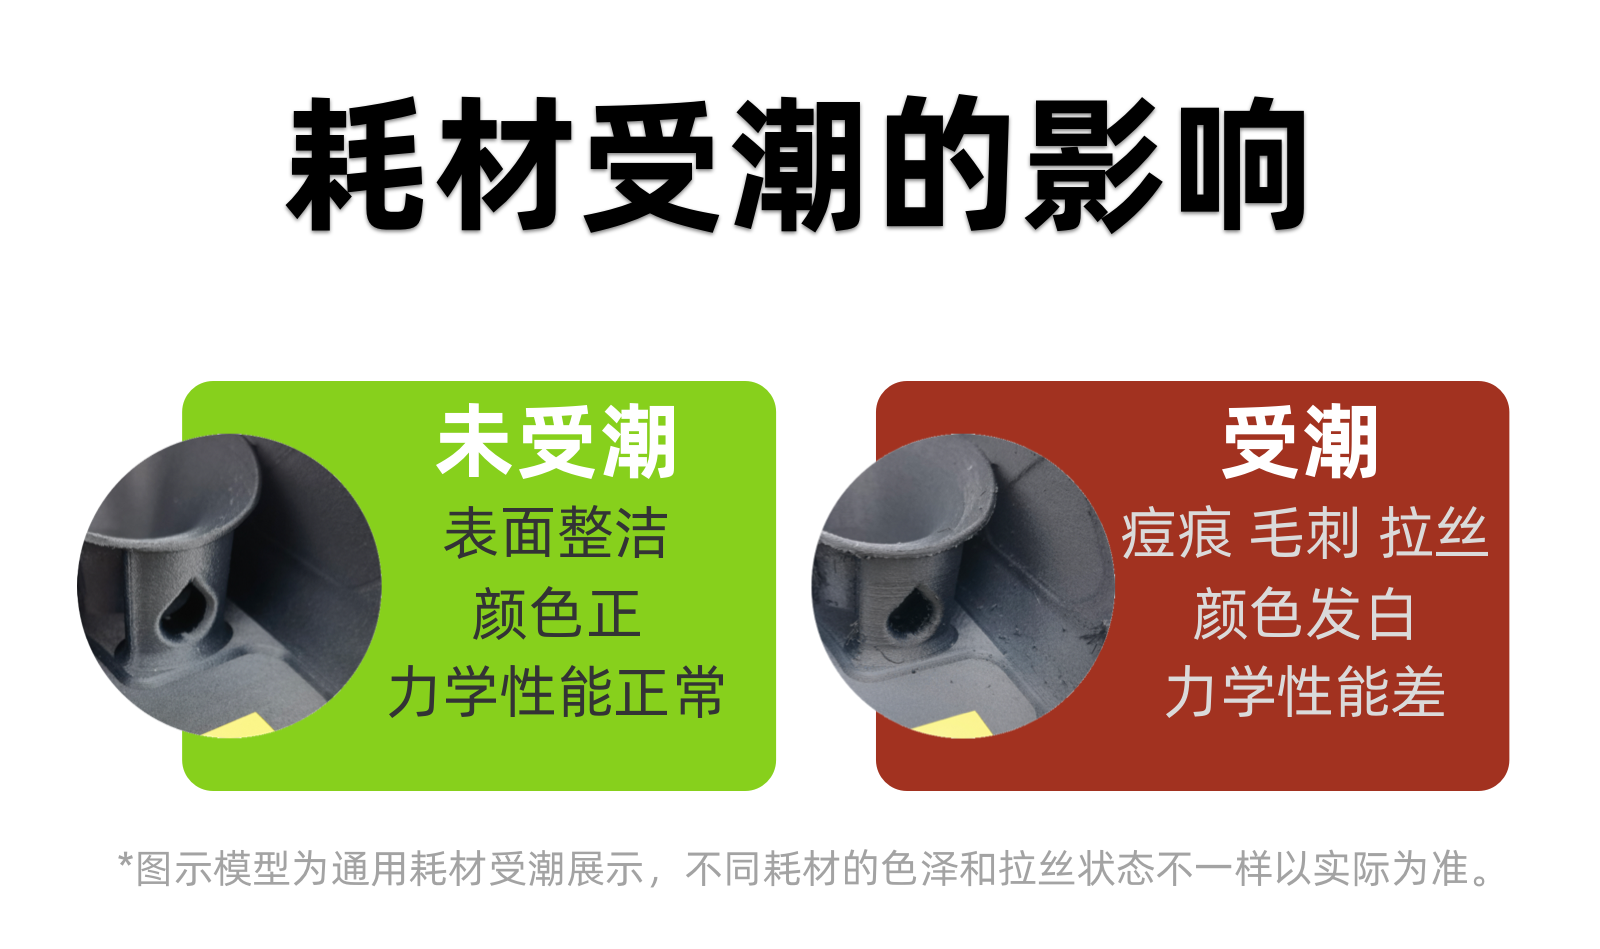 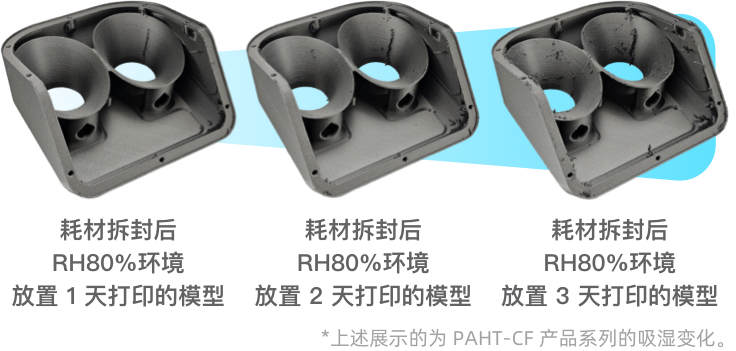 |
¶ Common spool dimensions, net weight, and specifications
| Spool material | The plastic spool material is PS - heat resistant up to 80℃.(Note: the temperature resistance of the spool is the upper limit, not equivalent to the drying temperature setting; refer to 'Filament Moisture Treatment Plan and Methods' for drying temperature) |
| Plastic spool size specifications |
|
| Product packaging instructions |
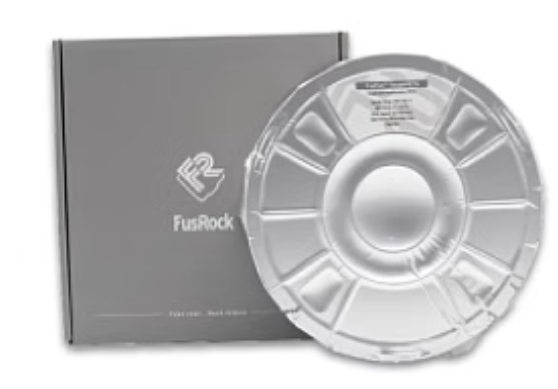 Double-sided aluminum foil bag: achieves efficient moisture-proofing, factory water content< 0.06 %, better water vapor barrier performance than transparent nylon bags. Built-in sealing strip:The heat-sealed bag can be torn open and reused, extending the dry state of the filament; it can serve as an eco-friendly storage bag. |
¶ Compatibility-related instructions for common 3D printers and related auxiliary equipment on the market
| 3D Printer compatibility list | List of supported Bambu Lab devices |
H2D\X1 Carbon\X 1\P1P\P1S\ (To ensure smooth feeding, it is recommended to use a dehumidifying box with bearings and feed the filament via a Teflon tube; recommend copper nozzles, recommendNozzle made of hardened steel or harder material; enclosure printing is recommended.; Supports AMS/AMS2, note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) A1/A1 mini (Ensure smooth feeding is essential; it is recommended to place in a dehumidifying box with bearings and feed into the printer using a Teflon tube; recommend copper nozzles, supportNozzle made of hardened steel or harder material; enclosure printing is recommended.; Supports AMS Lite series but not recommended, note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) Other to be supplemented |
| Fuzhi Equipment Support List |
Pro3/Pro3 Plus (Ensure smooth feeding is essential. It is recommended to use a moisture-proof box with bearings and feed via Teflon tube into the printer; recommend copper nozzle, recommendNozzle made of hardened steel or harder material; enclosure printing is recommended.; Note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) E2/E2-CF(Printing without sealing the box, pay attention to filament moisture protection.) Other to be supplemented |
|
| Creality |
K1/K1C/K1Max (Pay attention to the angle of the feed tube and adjust it to ensure smooth feeding; it is recommended to use a dehumidifying box with bearings and feed the filament via a Teflon tube; recommend copper nozzles, recommendNozzle made of hardened steel or harder material; enclosure printing is recommended.; Note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) Other to be supplemented |
|
| Prusa 3D |
Prusa XL (Note: adjust the angle of the feed tube to ensure smooth feeding is essential. It is recommended to use a moisture-proof box with bearings and feed via Teflon tube into the printer; recommend copper nozzle, recommendNozzle made of hardened steel or harder material; enclosure printing is recommended.; Note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) Other to be supplemented |
|
| Flashforge Technology |
AD5M (adjust the feed-tube angle as needed and ensure smooth filament feeding. A moisture-proof box equipped with bearings is recommended; feed the filament to the printer through a Teflon tube. Copper nozzles are recommended; it is recommendedNozzle made of hardened steel or harder material; enclosure printing is recommended.; Note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) Other to be supplemented |
|
| Qidi Technology QiDi | X-Max 3/Q1 Pro/X-Plus 3/X-Plus 4 (Note: The angle of the feed tube needs to be adjusted to ensure smooth feeding. It is recommended to use a dehumidifying box with bearings and send the filament into the printer using a Teflon tube; it is recommended to use a copper nozzle, and nozzles made of hardened steel or harder materials are supported;Nozzle made of hardened steel or harder material; enclosure printing is recommended.; Note moisture protection; external metal brackets are not recommended due to interference and risk of moisture absorption.) | |
| More support lists and descriptions | Send to [email protected] |
¶ Common issues
¶ Q: Looking forward to your questions~
¶ Analysis of customer case problems (demonstrating common problems encountered by customers one by one)
¶ Looking forward to your sharing!
¶ Health tip — Care for your health: FusRock recommends you
1, for long-term and large-scale use of 3D printing material, it is recommended to operate in a dedicated room with proper ventilation.
2, individuals with a history of allergies should confirm that the corresponding material used will not cause allergic reactions upon contact.
3 Friends with chronic respiratory diseases should wear masks to protect your health. Even if you do not have related diseases, it is strongly recommended to wear a mask during operation.
4. When sanding, cutting or otherwise processing finished fiber-filled prints in ways that may release fibers, take protective measures to prevent punctures or inhalation into the body. 5. Finally, keep printing operations away from children and infants to protect the environmental safety of the next generation.
¶ Application Disclaimer
1. Fusrock 3D printing filament is suitable for general printing applications and has been tested under standard conditions. However, the performance and safety of printed parts are influenced by various factors, including printing parameters, model design, usage environment, and actual application.
Using 2. with Fusrock material implies that the user is aware of and agrees to assess whether the printed part is suitable for their specific application, and assumes all risks arising therefrom.
3. Fusrock assumes no liability for any damage, injury, or loss that may result from the actual application of products printed using our filaments, including but not limited to structural failure, functional abnormalities, or safety hazards in the usage environment. Please conduct thorough testing before applying printed parts to critical, functional, or commercial scenarios. Except for materials explicitly certified by Fusrock, Fusrock products have not obtained certifications for medical, aerospace, or life-support systems.
4.FusRock filament is limited to civilian, non-weapon purposes, such as prototype development, hobby model making, and industrial component manufacturing. Any attempt to use the company's materials to manufacture firearms, airguns, or other controlled devices is strictly prohibited and violates the company's policy. 3D The use of printed products and their legal compliance are the sole responsibility of the end user.
¶ Disclaimer and Copyright
Thank you for visiting this website! Before using this website, please carefully read the following copyright statement and terms of use:
Copyright notice:
1. All content on this website, including but not limited to text, images, graphics, audio, video, software, and its compilation, code, and technical architecture (collectively referred to as "content"), is owned by this website or relevant rights holders and is protected by the Copyright Law of the People's Republic of China and other applicable laws and regulations.
2. Without written authorization from this website, no unit or individual may copy, reprint, disseminate, modify, display, adapt, mirror, upload, download, or otherwise use the content of this website in any form.
3. The copyright of third-party content cited on this website belongs to the original rights holders. If your legitimate rights and interests are infringed upon for reasons not attributable to this website, please contact us promptly; we will handle the matter immediately after verification.
Instructions for use:
1. You may non-commercially browse, download, or print content from this website in compliance with relevant laws and regulations and this statement, provided that you retain all relevant copyright notices and other ownership information. No modifications of any kind are permitted.
2. Commercial use of the content or services of this website is prohibited in any way, including but not limited to creating derivative works from the content, selling, or distributing to third parties.
3. The use of automated tools (such as crawlers, bots, etc.) to obtain, copy, monitor, or attempt to access the content or data of this website is prohibited.
Disclaimer:
1. This website strives to provide accurate and reliable information but makes no express or implied warranties regarding the completeness, timeliness, or accuracy of the content.
2. The website assumes no legal liability for any direct or indirect losses caused by the use of the content or services on this website.
3. This website may contain links to third-party websites, but this website assumes no responsibility for the content or actions of third-party websites.
Rights protection:
If you violate this statement and infringe upon the legitimate rights and interests of this website, we reserve the right to pursue legal liability, including but not limited to filing a lawsuit or taking other legal measures.
If you have any questions about this statement, please contact us via **[[email protected]]**.
The final right of interpretation of this statement belongs to this website.